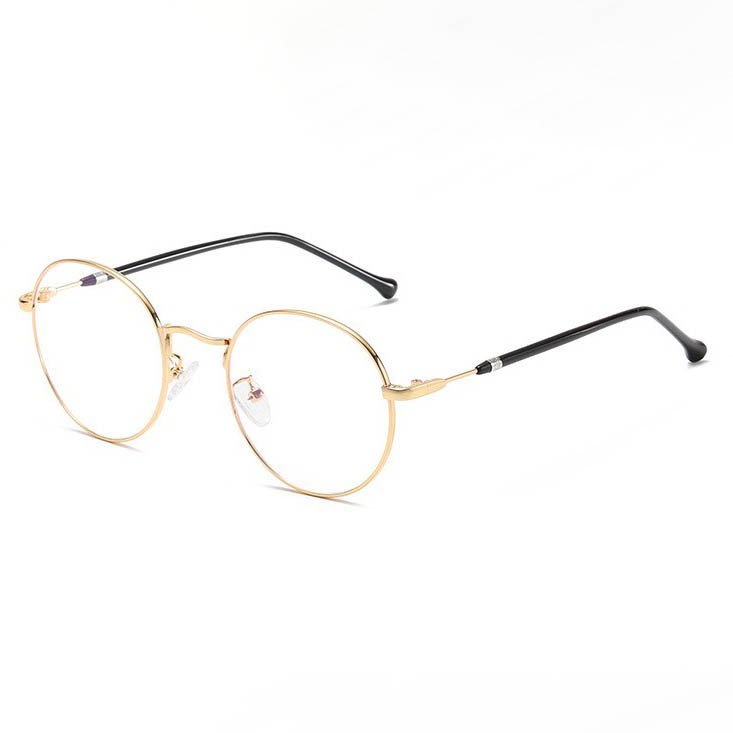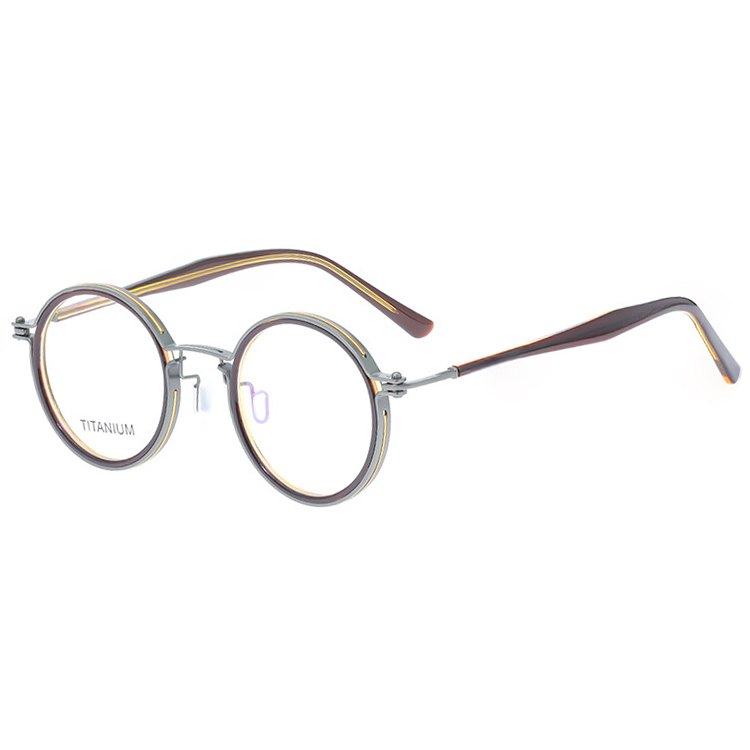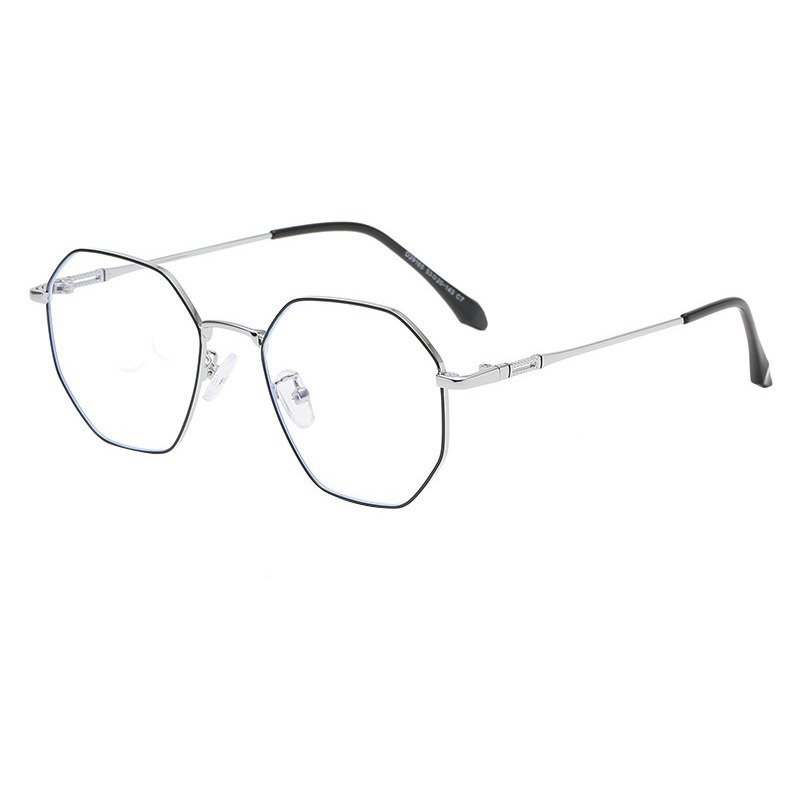
Boxed dimensions have to hold, the bridge has to sit on a nose without sliding, and the finish has to survive a lens being glazed into it. All three are decided before the frame is polished — which is why the drawing, the tool and the plating bath sit in the same building.
Metal first: monel (cupronickel) wire stamped, tumbled, polished and plated on our own line. Stainless where the rim has to be thin and stiff. Acetate blocks are cut and tumbled on the same benches as our sunglass fronts, so a colour approved on a sunglass programme can be matched on an optical frame.
Constructions: full-rim, semi-rimless with a nylon lower rim, and rimless with drilled lenses and polished edges. Temples are fitted with barrel or spring hinges, screwed to your drawing.
The count is small today — three frames in production — because optical is the line we are building out now. The tooling, the plating and the acetate bench are already here; what we are adding is shapes.